1 mm nozzle layer heights in ABS
Quick answer
A 1 mm nozzle prints usable layer heights from 0.25 mm to 0.75 mm, with 0.5 mm as the everyday default. Pair it with a line width of about 1.13 mm.
The quarter to three quarters window is the standard community rule. The hard limit is that a layer taller than the nozzle orifice cannot bond to the layer below.
| Layer height | Share of nozzle | Flow at 150 mm/s | Verdict |
|---|---|---|---|
| 0.25 mm | 25% | 42.2 mm3/s | Finer finish, slower |
| 0.38 mm | 38% | 64.1 mm3/s | Finer finish, slower |
| 0.5 mm | 50% | 84.4 mm3/s | Finer finish, slower |
| 0.68 mm | 68% | 114.8 mm3/s | Faster, coarser finish |
| 0.75 mm | 75% | 126.6 mm3/s | Faster, coarser finish |
Where the limits come from
The lower bound is practical: below about a quarter of the nozzle diameter, the extruder is being asked to meter such a thin line that small inconsistencies become visible, and the print time climbs steeply for detail you often cannot see. If you want finer layers than 0.25 mm, a smaller nozzle is the right answer rather than a thinner layer.
The upper bound is closer to physics. The nozzle tip presses each new layer into the one beneath it, and above roughly three quarters of the nozzle diameter it can no longer do that properly. The print still looks acceptable, but layer bonding falls away and the part splits along a layer line under load. Above the nozzle diameter itself, it cannot work at all.
What ABS adds
Warps badly in open air and emits styrene. Enclosure plus ventilation, not enclosure alone. With a 1 mm nozzle, ABS wants a nozzle temperature around 230 to 260 C and a bed at 95 to 110 C.
ABS needs an enclosure, and a larger nozzle makes that more true rather than less: thicker lines hold more heat and shrink harder as they cool, so warping gets worse as the nozzle grows. Extraction matters too, since this material emits VOCs and ultrafine particles that an enclosure concentrates rather than removes.
Nozzles and hotends
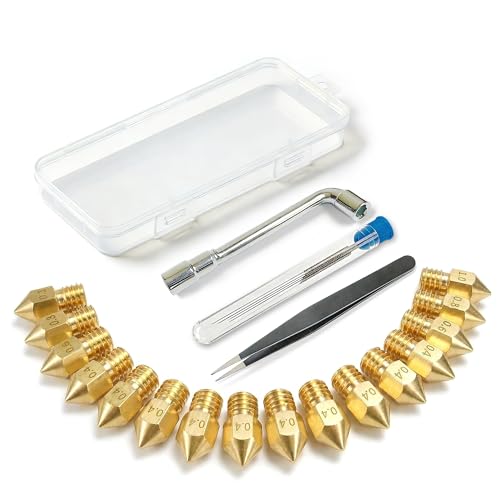
- LKNNEASTO
3D Printer Nozzle Kit, 16PCS MK8 Brass Nozzles 0.2/0.4/0.6/0.8/1.0mm
$7.19 Check pricePrices change often - Mudder
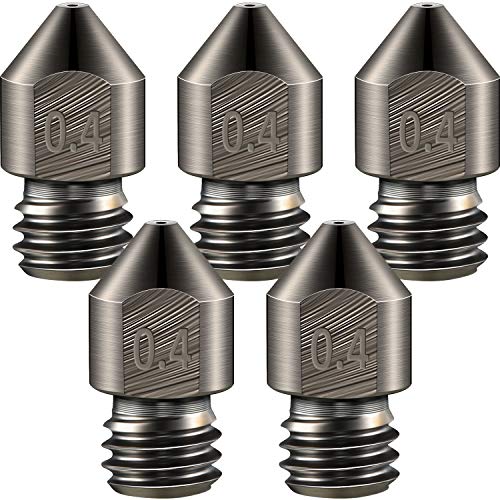
Mudder 5 Pcs Hardened Steel Nozzles 0.4mm Mk8 3D Printer Nozzles
$8.49 Check pricePrices change often - XIFOWE
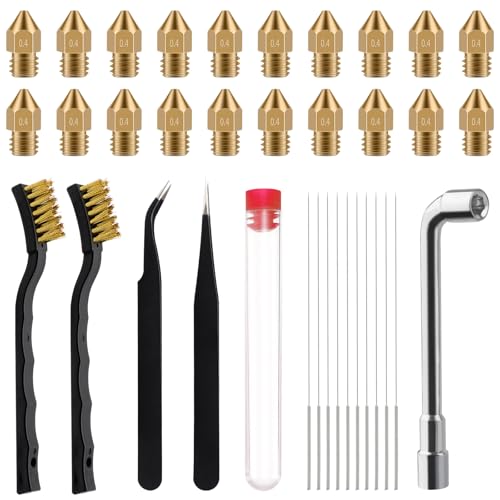
XIFOWE MK8 Nozzles 25 pcs 0.4mm 3D Printer Extruders Brass Nozzles
$9.99 Check pricePrices change often


Common questions
What layer height should I use with a 1 mm nozzle?
Start at 0.5 mm, which is half the nozzle diameter and sits in the middle of the usable 0.25 to 0.75 mm range. Drop toward 0.25 mm when a curved surface really matters, and rise toward 0.75 mm for chunky functional parts where speed is worth more than finish.
Is a 1 mm nozzle good for ABS?
Yes, and it is a large speed gain on solid parts, provided the hotend can feed it. A 1 mm nozzle at moderate speed demands several times the flow of a 0.4 mm one, so check that figure before assuming the speed is available.
Does a smaller layer height give finer detail?
Only vertically. Layer height controls how smooth a curve or slope looks as it rises, but horizontal detail such as a thin wall, a small hole or a crisp corner is set by the nozzle diameter and line width instead. If the detail problem is in the XY plane, a smaller nozzle helps and a thinner layer does not.
Why is my print weak even though it looks fine?
A layer height too close to the nozzle diameter is a frequent cause. The surface can look perfectly acceptable while each layer only lightly touches the one below, giving poor interlayer bonding and a part that splits along a layer line. Dropping to about half the nozzle diameter usually restores the strength.